Contact Us

Leanworx connects to the controllers on your CNC machines and shows what every machine is doing right now: running, idle or down, how many parts it has made, and why it stopped. No manual entry, no end-of-shift guesswork.
Works with Fanuc, Siemens, Mitsubishi, Haas and Brother controllers.
Used by manufacturers including TaeguTec India, SSS Springs, Zenith Precision and RBD Engineers.
Demo data for illustration.
Connects directly to the controllers already on your machines
CNC machine monitoring software collects data directly from a CNC machine's controller and shows it in real time: whether the machine is running, idle or stopped, how many parts it has made, its cycle times and the reasons for downtime. Manufacturers use it to measure OEE and utilization, cut downtime and replace manual production reports.
Most shops still track this on paper or in Excel. An operator writes down counts at the end of the shift, short stoppages get rounded off or forgotten, and the report reaches the manager the next morning, when it is too late to fix anything.
A CNC machine monitoring system takes the numbers straight from the machine. They are accurate, complete and available while the shift is still running, so supervisors can act on a problem in minutes instead of discovering it a day later.
One system for status, output, downtime and reporting, built for machine shops.
See every machine's state on one screen: running, idle, in setup or down. The status changes the moment a machine stops, so nobody has to walk the floor to find out.
Availability, performance and quality are calculated from real machine data for every machine, shift and day. Here is how the OEE formula works.
Every stoppage is logged with its exact start and end time. Operators tag the reason, such as tool change, no material or breakdown, so you can see which losses cost the most hours.
Compare available time with actual cutting time and find machines that look busy on paper but sit idle in practice. Read our guide to calculating machine utilization.
Part counts come straight from the controller, and actual cycle times are compared with the standard, so slow cycles and slow programs stand out.
Daily and hourly production reports are generated automatically, replacing the daily production report spreadsheets your team updates by hand.
Show live status and targets on any TV so operators and supervisors work from the same numbers. Learn more about the andon board.
Check any machine or plant from a browser or phone, in the office, at home or on the road, with remote machine monitoring.
Real screens from Leanworx: the same views your supervisors and managers use every shift.

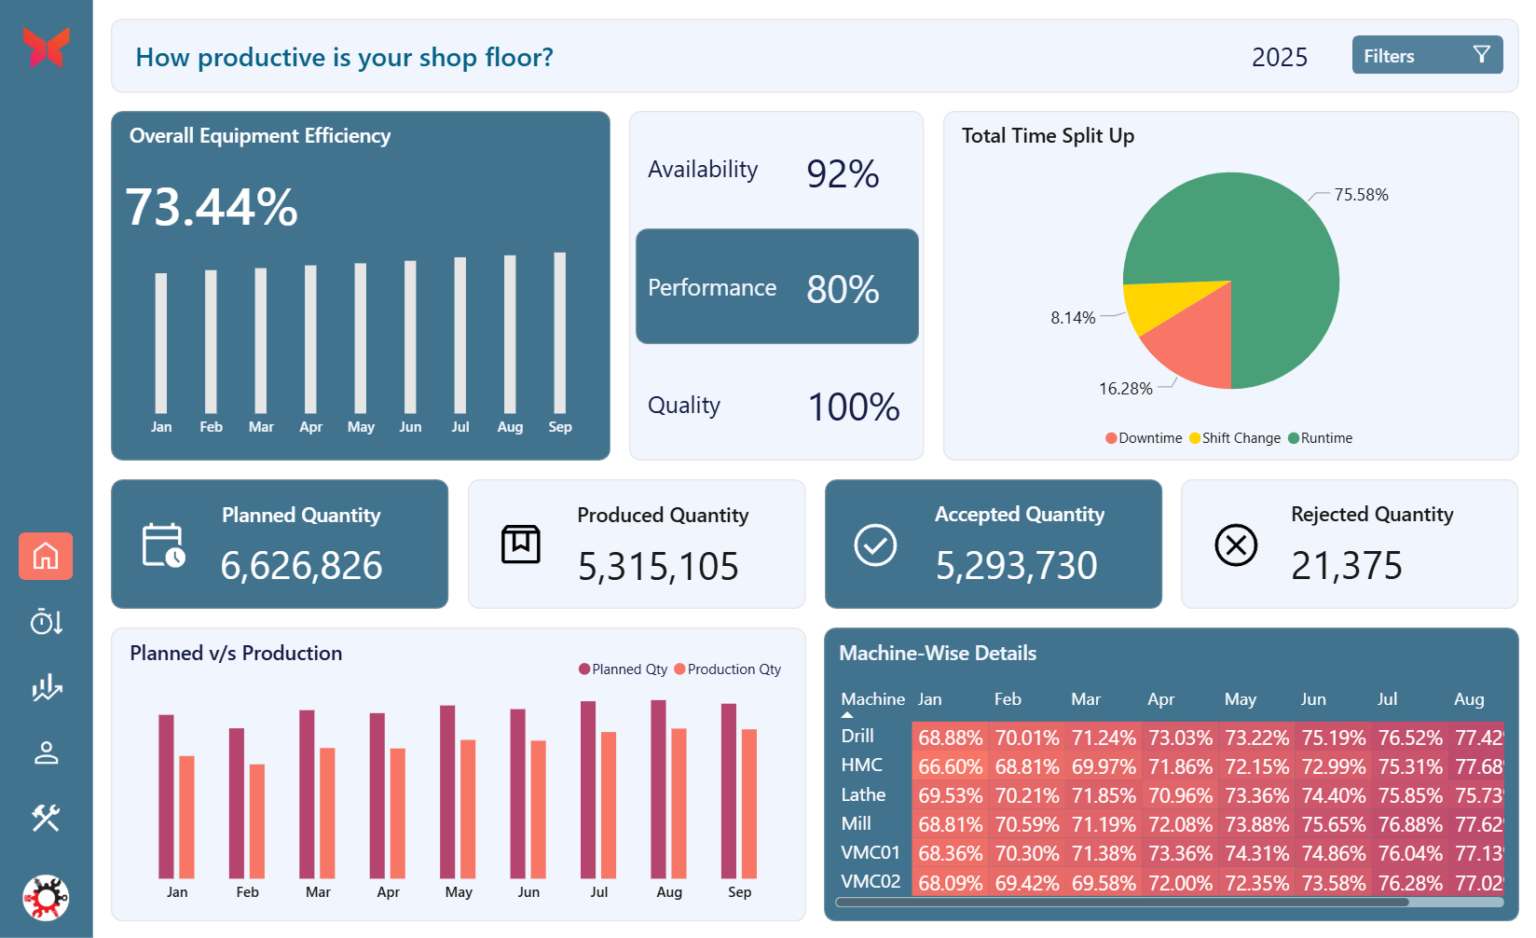
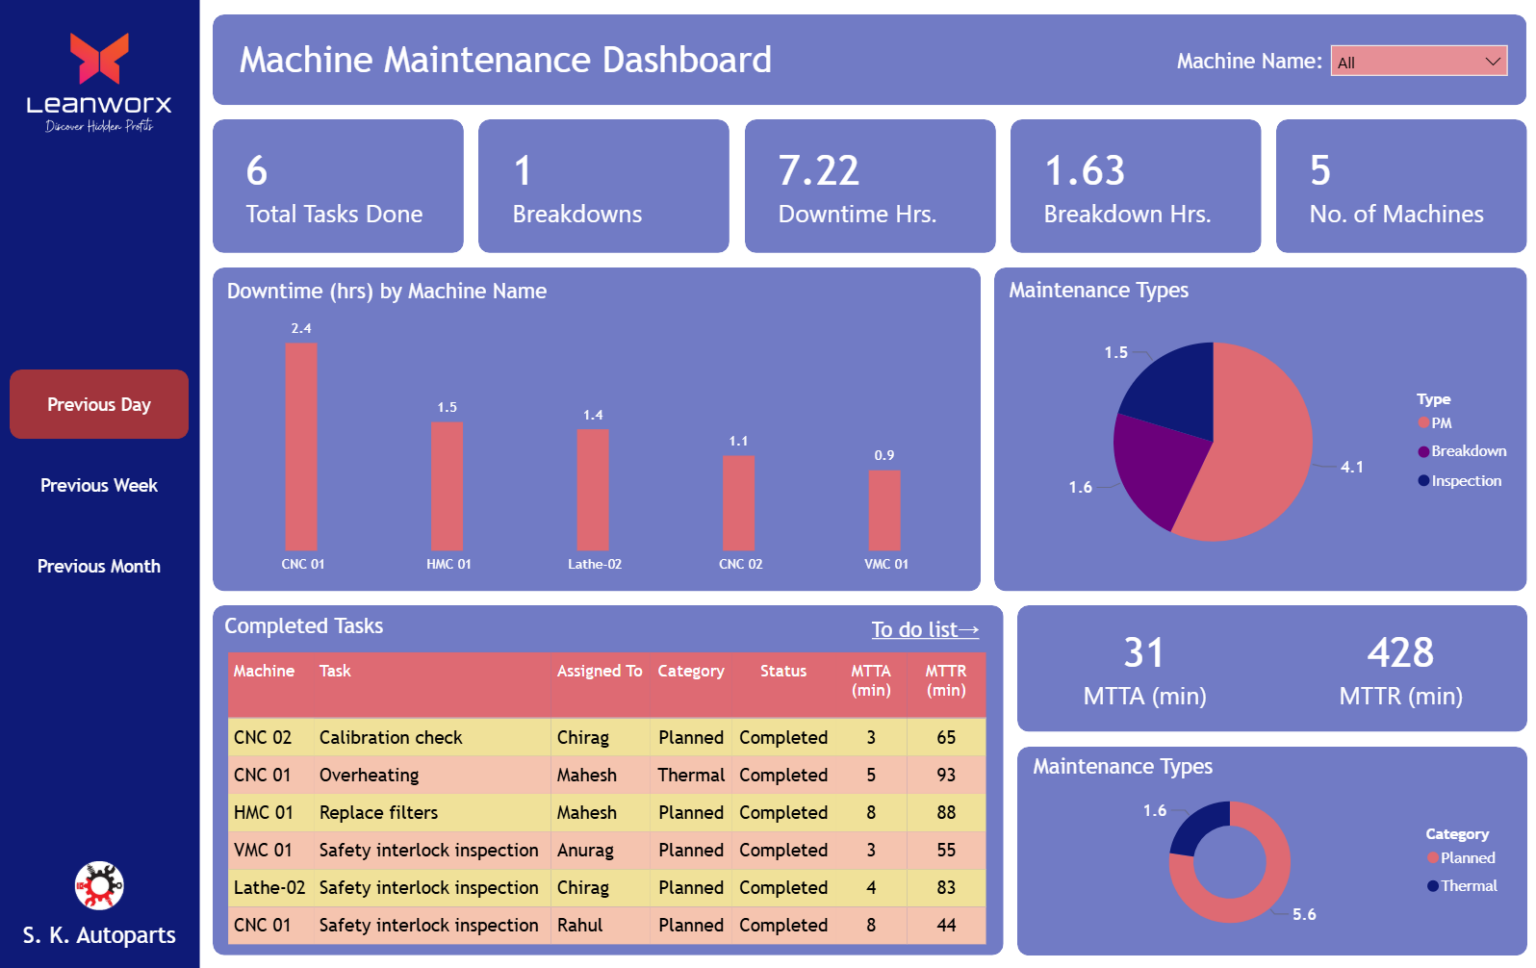
Three steps from a disconnected shop floor to live machine data.
Leanworx reads data from each machine's controller over your shop network. Your part programs and the way operators run the machine stay exactly the same. Older machines without a network port can be connected through an IoT device.
Status, part counts, cycle times and alarms are captured continuously on every shift, with no operator effort and no clipboard.
Dashboards, alerts and reports show where time is being lost, so supervisors can respond while the shift is running instead of after it ends.
Leanworx works with the controllers found on most CNC machines in job shops and production plants.
| Controller | Common on |
|---|---|
| Fanuc | VMCs, HMCs and turning centres from most Indian and global machine builders |
| Siemens Sinumerik | Machining and turning centres from European and Indian builders |
| Mitsubishi | VMCs, turning centres and Japanese-built machines |
| Haas | Haas vertical and horizontal machining centres and lathes |
| Brother | Brother high-speed tapping and drilling centres |
| Older machines | Machines without a network-ready controller, connected through an IoT device |
Setup guides by machine brand: Haas, Mazak, DMG Mori, Makino, LMW, Jyoti, Ace Micromatic, BFW and Tsugami. Not sure about your machine? Tell us the controller model when you sign up and we will confirm.
Why shops that move from paper and Excel to a machine monitoring system rarely go back.
| Paper and Excel | Leanworx | |
|---|---|---|
| Where data comes from | Operator notes and memory | Directly from the CNC controller |
| Downtime | Rounded off, short stops often missing | Every stoppage, with exact start and end time |
| When you see it | Next morning | Live, during the shift |
| OEE | Calculated by hand, if at all | Automatic for every machine, shift and day |
| Reports | Someone's time, every shift | Generated automatically |
| Trust in the numbers | Depends on who filled it in | Same method, every machine, every time |
A Leanworx customer replaced end-of-shift breakdown reports with live data from their CNC machines and cut unscheduled breakdowns by 28%. Read the case study.
Results from machine shops and plants using Leanworx CNC machine monitoring every day.
We've seen a lot of OEE improvements because now we can understand the parts, the spindle runtime, how effectively we are running. It's actually helped us to move from 3 shifts down to 2 shifts with more output. So we've moved from about 30% spindle utilization to now over 55% spindle utilization.
25% less night-shift downtime
Our downtime has decreased by 10%. The downtime, especially in the night shift, has reduced by more than 25%, which is a very, very important thing for us and is contributing a lot towards our productivity.
30% less machine downtime
With Leanworx we have been able to bring down our machine downtime by about 30% and increase in OEE by 10 to 15%, which is a huge saving. We have been getting fantastic results out of it. The reports that we generate every morning give us a good insight on the productivity and the performance of the operator as well as the machine.
10 to 12% more production
Overall, I see at least 8 to 10% efficiency improvement, especially OEE and the spindle run time. Setup time has been reduced and we can see an improvement of at least 10 to 12% production improvement.
10 minutes to connect a machine
It takes hardly 10 minutes for a person to connect to the machine. I can tell you that we are able to reduce the downtime, and we are able to improve productivity. The middle level supervisors and managers are also satisfied with the exact data that they are getting from the Leanworx system.
No more arguing about the data
After implementing Leanworx we are no longer discussing the quality of data or accuracy of data. Discussion revolves around what can be done to improve productivity. Looking at the benefit of utilizing and improving the equipment utilization, the incremental cost that we incur by paying the subscription is very small and it's a good value proposition from our point of view.
OEE they can actually trust
When a customer asks, what is your OEE? We say 85%. Are we really at 85%? I don't think so. After installing Leanworx and improving systems, it's 88 when we finally checked the last time. So that's a substantial advantage.
Leanworx Lite gives smaller shops live machine status, OEE and automatic reports without needing an IT team. Start free and connect your first machines yourself.
Try Leanworx free See plans and pricingFor 20 or more machines, or several plants, our team plans the rollout with you and sets up dashboards for production, maintenance and management.
Book a walkthroughIt reads data from your CNC controllers and shows each machine's status, part counts, cycle times and downtime in real time. It also calculates OEE and utilization and produces production reports automatically.
Leanworx supports Fanuc, Siemens, Mitsubishi, Haas and Brother controllers. Older machines without a network-ready controller can be connected through an IoT device. Share your controller model and we will confirm compatibility.
No. Leanworx reads data from the controller. It does not change your part programs or the way operators run the machine.
A machine monitoring system focuses on what the machines are doing: status, output, downtime and OEE. An MES covers wider processes such as scheduling, inventory and quality records. Many shops start with machine monitoring because it is quicker to set up and shows results sooner.
Usually minutes, not days. As Gurpreet Singh, MD of Pal Shell Cast, puts it: "It takes hardly 10 minutes for a person to connect to the machine."
Yes. Leanworx runs in the browser, so you can check machine status and reports on a phone, tablet or computer from anywhere.
Every stoppage is recorded with its exact duration and reason, so you can see which causes cost the most time and fix those first. Leanworx customers report results such as 30% less machine downtime at RBD Engineers and over 25% less night-shift downtime at Zenith Precision.
Yes. You can try Leanworx free on your own machines. Start from the Try for Free page.
Yes. Small shops often feel lost machine hours the most. Leanworx Lite is designed for job shops with a few machines and no dedicated IT team.
Connect a machine and see its real status, output and downtime. Your programs stay exactly as they are.
Try Leanworx free